Computational and Physical Simulation Methods for Off-Line Validation of Soft Magnetic Composite Impeder Performance
Yi Zhou, Daniel Günther, Igor Niedzwiecki, Martin Kroll, Egbert Baake, and Robert C. Goldstein
Resources
74 papers, articles and presentations on magnetic flux control, simulation, induction hardening, welding and more, with downloadable PDFs.
74 of 74 shown · Books · Patents
Yi Zhou, Daniel Günther, Igor Niedzwiecki, Martin Kroll, Egbert Baake, and Robert C. Goldstein
Robert C. Goldstein, D. Scott Mackenzie, Sean Muyskens, Sahadev Khatri · Fluxtrol Inc. Auburn Hills, USA; Quaker Houghton, Conshohocken, PA
Rob Goldstein and Sean Muyskens
Alec Williamson, Samuel Findley, Dominic Piccone, Colton Brown, Sam Nikolai, David Ulrich, Garrison Hommer, Rob Goldstein, Matthew McCosby, David Barbier, Laurent Lesne, Eliseo Hernandez, Malavikha Rajivmoorthy, Emmanuel De Moor, Lawrence Cho
Sean Muyskens and Rob Goldstein FASM
Sean M. Muyskens, David R. Morris, Christopher J. Yakey and Robert C. Goldstein · HES 2023 Padua, Italy
Sean M. Muyskens, Robert C. Goldstein · IMAT 2023 Detroit, Michigan
Robert Cryderman, Finn Bamrud, Tareq Eddir, and Robert GoldsteinPublication: Journal of Materials Engineering and Performance, 2023
Sean M. Muyskens, Robert C. Goldstein · IMAT 2022 New Orleans, Louisiana
Sean M. Muyskens, Tareq I. Eddir, Robert C. Goldstein · ASM HTS Heat Treat 2021 St. Louis, Missouri
Robert Cryderman (Colorado School of Mines), Finn Bamrud (Colorado School of Mines), Tareq Eddir (Fluxtrol Inc.), Robert C. Goldstein (Fluxtrol Inc.) · ASM HTS Heat Treat 2021 St. Louis, Missouri
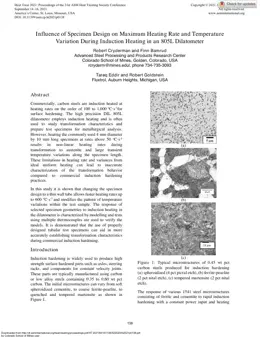
Commercially, carbon steels are induction heated at heating rates on the order of 100 to 1,000 °C·s-1 for surface hardening. The high precision DIL 805L dilatometer employs induction heating and is often used to study transformation characteristics and prepare test specimens for metallurgical analysis. However, heating the commonly used 4 mm diameter by 10 mm long specimens at rates above 50 °C·s-1 results in non-linear heating rates during transformation to austenite and large transient temperature variations along the specimen length. These limitations in heating rate and variances from ideal uniform heating can lead to inaccurate characterization of the transformation behavior compared to commercial induction hardening practices.
In this study it is shown that changing the specimen design to a thin wall tube allows faster heating rates up to 600 °C·s-1 and modifies the pattern of temperature variations within the test sample. The response of selected specimen geometries to induction heating in the dilatometer is characterized by modelling and tests using multiple thermocouples are used to verify the models. It is demonstrated that the use of properly designed tubular test specimens can aid in more accurately establishing transformation characteristics during commercial induction hardening.
Tareq Eddir (Fluxtrol Inc.), Robert C. Goldstein (Fluxtrol Inc.), Robert Haun (Anspanner LLC) · IMAT 2021 St. Louis, Missouri
Sean M. Muyskens, Robert C. Goldstein · IMAT 2021 St. Louis, Missouri
Induction tube welding is used for the continuous production of metallic tubes. These systems often utilize an internal magnetic flux controller (impeder) to improve process efficiency. Significant energy savings and increased productivity have been demonstrated both theoretically and practically when switching from the traditional ferrite impeder core, to one made of a soft magnetic composite (SMC) with high saturation flux density. In order to use SMCs in these systems it is important to balance the greater heat generated in these materials at higher fields with the cooling water available.
A test stand was devised for physical simulation of SMC impeder performance for use in induction tube welding systems. Tests were run to determine the loading and cooling conditions that an impeder core made of SMCs could survive. Additionally, loss estimates based on the rise in temperature from the cooling water were compared with published loss data for the SMCs used. The goal of these tests was to create a design envelope in which impeder cores made of SMCs could survive and validate their use in induction tube welding systems.
Tareq Eddir (Fluxtrol Inc.), Robert C. Goldstein (Fluxtrol Inc.), Robert Haun (Anspanner LLC) · UIE 2021 Pilsen, Czech Republic
Sean M. Muyskens, Robert C. Goldstein · UIE 2021 Pilsen, Czech Republic
Induction tube welding is used for the continuous production of metallic tubes. These systems often utilize an internal magnetic flux controller (impeder) to improve process efficiency. Significant energy savings and increased productivity have been demonstrated both theoretically and practically when switching from the traditional ferrite impeder core, to one made of a soft magnetic composite (SMC) with high saturation flux density. In order to use SMCs in these systems it is important to balance the greater heat generated in these materials at higher fields with the cooling water available.
A test stand was devised for physical simulation of SMC impeder performance for use in induction tube welding systems. Tests were run to determine the loading and cooling conditions that an impeder core made of SMCs could survive. Additionally, loss estimates based on the rise in temperature from the cooling water were compared with published loss data for the SMCs used. The goal of these tests was to create a design envelope in which impeder cores made of SMCs could survive and validate their use in induction tube welding systems.
Prem Vaishnava, Mitchel Madeira, Doug Whittaker, Robert C. Goldstein · ASM HTS Heat Treat 2019 Detroit, Michigan
Soft Magnetic Composites (SMCs) are widely used in Induction Heat Treating (IHT) applications to increase system efficiency, improving heat pattern control, and preventing undesired heating of adjacent areas of the work piece or machine components. SMCs consist of soft magnetic particles, individually insulated from one another by organic and/or inorganic materials. In most induction heat treating applications, the lifetime of an inductor is limited by the fatigue life of the copper. In severe applications, the lifetime is also limited by the lifetime of the magnetic flux controller. The typical source of failure in magnetic flux controller is corrosion caused by elevated temperature and exposure to the oxidizing agent such as quenchants and air surrounding the induction coil.
Coating SMCs can modify their surface properties and significantly enhance their corrosion resistance. In this paper, we have coated four commercially available SMCs with ceramic polymer-based coating materials with different surface preparation techniques. ASTM D1735 humidity test was performed for 168 hours. We found that with proper coating technology, the materials do not show degradation during the standardized testing.
Sean M. Muyskens, Tareq I. Eddir, Robert C. Goldstein · ASM HTS Heat Treat 2019 Detroit, Michigan
Inductive welding is a popular method for making metallic tubes used in a variety of industries. A majority of these induction tube welding systems use internal magnetic flux controllers (impeders) to limit the current flowing on the ID of the tube under the induction coil. As higher power, solid state IGBT power supplies become more widely available for tube welding, and demand for lower cost tubes with higher strength to weight ratios increases, magnetic loading of these impeders is also increasing. Traditionally, impeders are made of ferrites which have a low saturation flux density and can become saturated in these demanding conditions. Saturation of the impeder results in greater currents on the tube ID and lower process efficiency and weld quality. In order to expand the upper operating range of these more demanding systems while maintaining the weld quality, a change in impeder material from ferrites to soft magnetic composites (SMC) with greater saturation flux densities is suggested, as well as the addition of external magnetic controllers (bridges).
In this paper, a comparison is made between induction systems with impeders constructed from traditional ferrites and those utilizing bridges and impeders made from SMCs. To do this, a simulation study will be used to estimate impeder flux density, required coil current, and temperature distribution at the end of heating when using impeders made of the two materials, with and without bridges. By soft coupling 3-D electromagnetic models with 2-D electromagnetic and thermal models, a fast and accurate depiction of the welding process can be achieved. A case study is presented comparing simulation results to experimental results.
Andrew L. Banka (Airflow Sciences Corporation), Robert C. Goldstein (Fluxtrol Inc.), Robert L. Cryderman (Colorado School of Mines), Tareq Eddir (Fluxtrol Inc.), Andrew Senita (Airflow Sciences Corporation) · ASM HTS Heat Treat 2019 Detroit, Michigan
Dilatometry test systems are commonly used for characterizing the transformation behavior in steels using induction heating for the heating source and gas flow for the cooling source. In these systems, the steel test article is assumed to have a uniform temperature throughout the sample. The accuracy of this assumption depends on the design of the induction heating and gas cooling systems, as well as the time scales for heating and cooling. Previous papers by the authors have shown the variations in temperature that occur during heating and cooling for a TA Instruments DIL805 dilatometer (dilatometer).
Investigations were carried out for development of an improved heating/cooling system for this dilatometer using electromagnetic and thermal analyses for the induction coil and CFD analyses for the high-pressure gas cooling system. Electromagnetic analyses showed that a novel cooling system could be incorporated, though higher power would be required to maintain the same heating rate. While the improved cooling system showed promise on an idealized basis, full CFD modeling shows that the system would not provide improved cooling due to complex flow dynamics.
Sean M. Muyskens, Tareq I. Eddir, Robert C. Goldstein · HES 19 Padova, ItalyPublished Journal: COMPEL, 2019
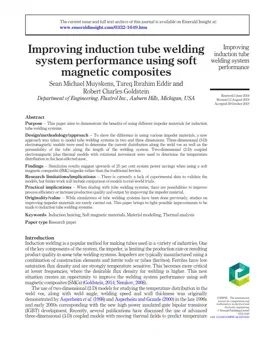
Sean M. Muyskens, Tareq I. Eddir, Robert C. GoldsteinPublication: COMPEL, 2019
Purpose: This paper aims to demonstrate the benefits of using different impeder materials for induction tube welding systems.
Design/methodology/approach: To show the difference in using various impeder materials, a new approach was taken to model tube welding systems in two and three dimensions. Three-dimensional (3-D) electromagnetic models were used to determine the current distribution along the weld vee as well as the permeability of the tube along the length of the welding system. Two-dimensional (2-D) coupled electromagnetic plus thermal models with rotational movement were used to determine the temperature distribution in the heat-affected zone.
Findings: Simulation results suggest upwards of 25 percent system power savings when using a soft magnetic composite (SMC) impeder rather than the traditional ferrites.
Research limitations/implications: There is currently a lack of experimental data to validate the models, but future work will include comparison of models to real-world trials.
Practical implications: When dealing with tube welding systems, there are possibilities to improve process efficiency or increase production quality and output by improving the impeder material.
Originality/value: While simulations of tube welding systems have been done previously, studies on improving impeder materials are rarely carried out. This paper brings to light possible improvements to be made to induction tube welding systems.
Keywords: Induction heating, Soft magnetic materials, Material modeling, Thermal analysis
Paper type: Research Paper
Prem P. Vaishnava, Robert C. Goldstein · HES 19 Padova, Italy
Tareq Eddir, Robert Goldstein, Ethan Buchner, Emmanuel De Moor, Robert Cryderman · IFHTSE TPIM 18 Spartanburg, South Carolina
Dilatometry test systems are commonly used for characterizing the transformation behavior in steels and induction heating is frequently selected as the heating source. In these systems, the steel test specimen is assumed to have a uniform temperature throughout the sample. This is a good assumption for slow heating rates with small specimens, however, for induction hardening heating rates this may not be accurate. Using computer models, it is possible to predict the temperature dynamics of the sample, both radially and axially, during heating.
O1 tool steel in the quenched condition was utilized to characterize and model heating temperature gradients. The case of a 50°C/s heating rate was presented previously [1]. In this study, specimens instrumented with multiple thermocouples were induction heated at rates up to 500 °C/s. The test data and geometry were evaluated with 2-D models to characterize transient temperature gradients. The goal of the modeling is to better characterize temperature corrections required when rapid heating is used to determine transformation behavior during rapid induction heating. This paper presents the data for faster heating rates and quantifies the impact of the different heating rates on the dynamic temperature distributions in the sample.
Bernd-Arno Behrens, Robert Goldstein, Anna Chugreeva · IFHTSE TPIM 18 Spartanburg, South Carolina
Bernd-Arno Behrens, Robert Goldstein, David Guisbert, Deniz Duran · IFHTSE TPIM 18 Spartanburg, South Carolina
Bi-material machine components are fabricated usually by joining two individual components which are already given their near-final or final form. These are then put into operation either directly or upon a finishing process. Contrary to that, researchers of the Collaborative Research Centre “CRC 1153” Tailored Forming are investigating novel process chains, in which different materials are joined in the first step and then subjected to further processing, i.e., forming, machining and heat treatment. By this means, the joining zone properties, which are adversely affected due to the joining process, can be treated and improved via thermomechanical processing during forming. On the other hand, process-specific challenges arise especially for workpieces consisting of dissimilar materials, i.e., steel and aluminum. In order to obtain a favorable flow behavior of the materials in the vicinity of the joining zone, a near step-function temperature distribution in the bi-material billet is desirable. Induction heating is viewed as the most promising method to be used for this purpose.
At the Heat Treat 2017 conferences, a paper was presented which discussed the strategy for thermomechanical processing and the modeling of the first concept for the induction heating process [1]. The current study builds on the previous paper and presents the modeling of the forming process along with the analysis of the first prototype samples formed using the technology. A metallurgical evaluation of the joining zone properties of the prototype components after thermomechanical processing will be presented. Additional considerations will be given on how to further improve the process and move towards a production capable process.
Robert Goldstein · ASM HTS 17 Cleveland, OH
Robert Goldstein · 2017 Colorado School of Mines
Robert Goldstein, Robert Cryderman · UIE Congress Hannover, Germany
Lee M. Rothleutner, Chester J. Van Tyne, Robert Goldstein, John Jackowski, and Greg Fett · HT 2017
Robert Goldstein, Ethan Buchner, Robert Cryderman · Colorado School of Mines
Dilatometry test systems are commonly used for characterizing the transformation behavior in steels and induction heating is commonly the heating source. In these systems, the steel test article is assumed to have a uniform temperature throughout the sample. This is a good assumption for slow heating rates with small samples, however, for induction hardening cycles this may or may not be accurate. Using computer models, it is possible to predict the temperature dynamics of the sample, both radially and axially, during the thermal processing cycle (heating and cooling).
O1 tool steel was utilized to characterize and model heating and cooling temperature gradients. Specimens instrumented with multiple thermocouples were induction heated and gas quenched. The test data and geometry were evaluated with 1-D and 2-D models to characterize transient temperature gradients. The goal of the modeling is to better characterize temperature corrections required when rapid heating and cooling processes are used to determine transformation behavior in induction hardenable steels.
Robert Goldstein, Bernd-Arno Behrens, Deniz Duran · ASM HTS 17 Cleveland, OH
Robert Goldstein, Valentin NemkovPublication: IEEE COMPEL, 2017
Purpose – Effect of unstable “wavy” temperature distribution on the part surface during the process of induction heating of ferromagnetic materials was observed and reported by two Russian scientists in 1940 (Babat and Lozinskii, 1940). They reported that under certain conditions, one can observe periodical or quasi-periodical bright stripes on the part surface when its temperature passes through the Curie point. In time, these stripes expand and merge, forming a normal temperature pattern. They called this phenomenon “polosatiy nagrev” (striation heating). Let us call it the “zebra effect” for simplicity. It can exist for a relatively long time, from several seconds to several tens of seconds. Several explanations of the zebra effect were proposed with not very convincing arguments.
Design/methodology/approach – Wider spreading of induction technology and use of computer simulation of induction processes create a demand and open new possibilities for study of the zebra effect. This study provides an overview of the available information about the zebra effect and gives new explanation of this phenomenon based on existing experimental data and new results of simulation. Conditions for zebra occurrence and its technological importance or limitations are discussed.
Findings – Computer simulation using the Flux 2D program allows to demonstrate the striation (zebra) effect that can appear in the process of heating magnetic materials and reproduce main experimental findings related to this effect. Simulation provides a great opportunity to investigate the zebra phenomenon in virtual reality, providing qualitatively correct results. Results of simulation show that the zebra effect can appear in a relatively narrow range of material properties and operating conditions. The main factor is a big enough gradient of permeability near the Curie point. At present, it is difficult to expect high quantitative accuracy of simulation due to multiple assumptions in simulation algorithms and insufficient or inaccurate information about the material properties near the Curie point.
Originality/value – Several explanations of the zebra effect were proposed with not very convincing arguments. There were concerns that the zebra effect could set significant limits on the use of induction heating for surface hardening due to non-uniform temperature distribution along the part (Babat and Lozinskii, 1940; Babat, 1965; Lozinskii, 1949, 1969). However, it did not happen. There were no complaints from scientists or practitioners regarding any negative effect of the zebra phenomenon. Moreover, the authors of this paper did not find any original publications on this issue for more than half a century. Only few old induction experts confirm that they observed the zebra effect or something similar, whereas a great majority of induction community members never heard about it.
Keywords – Computer simulation, Induction heating, Electromagnetic induction, Curie point
Paper type – Technical paper
B. M. Whitley, J. G. Speer, R. L. Cryderman, R. C. Goldstein, K. O. Findley and D. K. Matlock · Thermec 2016 Graz, AustriaKeywords: thermomechanical processing, microalloy, austenite conditioning, induction hardening, physical simulation, hot torsion, prior austenite grain size
Bulent Chavdar, Robert Goldstein, Lynn Ferguson · IFHTSE 2016 Savannah, GA
Feasibility of making lightweight powertrain products with hot hydroforging of steel/low density material hybrid billets is explored. A bimaterial billet is designed such that a steel wall encloses a low density core 100%. Furthermore the low density core is selected among the materials that have lower melting or softening temperature than steel such as aluminum and glass. In hot hydroforging the bimaterial billet is heated to 1000-1200 C range similar to the conventional hot forging of steel. However, in hot hydroforging the core is in liquid or viscous state while steel shell is in solid state similar to the conventional hydroforming. During hot hydroforging the viscous/liquid core has negligible resistance to flow thereby providing a uniform hydrostatic pressure inside the steel and enabling a uniform deformation of the solid steel wall.
Steel/aluminum bimetal billets were prepared. Then, the bimetal billets were hot hydroforged in closed dies in one blow. A uniform steel wall thickness was observed all around the forged part upon cross sectioning. However, there was also a large shrinkage void in the aluminum core. The large shrinkage void is formed due to the CTE mismatch between steel and aluminum and the volume increase of aluminum during phase change. The large shrinkage void can be eliminated if aluminum is replaced by glass that has a matching CTE to that of steel. Furthermore, glass does not have to be fully melted at forging temperatures thereby mitigating the risks of phase change. On the other hand the molten aluminum core can be emptied out of steel shell after forging thereby giving rise to the novel concept of “investment forging”. A hollow part with uniform steel shell can be formed for the ultimate weight and cost reductions. For example investment forging of hollow steel valves for engine applications is feasible by hot hydroforging.
Robert Goldstein, Dr. Valentin Nemkov, Dr. Lynn Ferguson, Dr. Zhichao Li · MS&T 2016
Robert Goldstein, Bulent Chavdar, Lynn Ferguson · IFHTSE 2016 Savannah, GA
Recently, a concept to produce lightweight products by hot forging a steel shell that had a lightweight core was presented that could lead to component weight savings up to 50%. Some targeted products are gears, valves, and flanges. The steel shell is envisioned to carry most of the load in a target application while the lightweight core serves as a space holder during the forming process. After forming, the lightweight material may either remain in the component and contribute to the load carrying capacity, or be emptied out to achieve the ultimate weight reduction.
In this paper, the concept studied is hot forged from a bimetal billet, which is a steel tube press fit with a solid aluminum core and welded shut with steel end caps. For the experimental part of the studies Al 7075 was selected as the core material due to its high strength to weight ratio and 1020 steel was selected because of its availability as a tube. Induction heating was selected as the heating method for bimetal forging. This is due to the ability of induction heating to rapidly heat the steel layer. Successful bimetal forging of a closed vessel requires the steel layer to be in the austenite phase prior to the aluminum reaching high temperatures to prevent compromising the weld seams. Modeling of the induction heating process is complex due to the dimensional movement of components during the process. A method was developed to accurately model the induction heating process and predict power requirements. The method will be described and the results of the models will be compared to experimental findings. The forming process will be discussed in another paper at the conference. The simulation presented is for solid state forging of a steel aluminum billet, but the method for modeling the process is the same for hot hydroforging or other material combinations.
Robert Goldstein, Valentin Nemkov · HES 2016 Padua, Italy
C. Yakey, V. Nemkov, R. Goldstein, J. Jackowski · ASM HTS 15 Detroit, MI
John K. Jackowski, Robert C. Goldstein, Valentin S. Nemkov · Aeromat 2015
Zhichao (Charlie), B. Lynn Ferguson, V. Nemkov, Robert Goldstein, John Jackowski, and Greg Fett · ASM HTS 15 Detroit, MI
Bulent Chavdar, Robert Goldstein, Xi Yang, Jacob Butkovich, Lynn Ferguson · IDE 15 Bremen, Germany
V. Nemkov · EPM 15 Cannes, France
Computer simulation is a widely accepted tool for design of induction coils and other components of induction systems, for development of new processes and equipment, for troubleshooting and for teaching and learning. Multiple programs and packages are being used for these purposes, from “home-made” programs to multiphysics packages such as Comsol, Ansys or Flux. One of the first questions, asked by new users, is: “How accurate are the results?”. The author has long experience in computer simulation and design of various induction systems and understands well that there is no simple answer to this question.
This presentation is an attempt to discuss the sources of inaccuracies and provide information on what the user must pay attention to. It may be useful for the software users and developers as well as for all users of induction heating. The study is related to induction heating itself, i.e. to electromagnetic and thermal processes with much less attention to other processes. Simulation of structural transformations, stresses and deformations as well as electromagnetic forces and magnetohydrodynamic processes are not considered in this presentation.
R. Goldstein, W. Stuehr and M. BlackPublication: ASM International, 2014
John K. Jackowski, Robert C. Goldstein, Valentin S. Nemkov · SAMPE 14 Seattle, WA
V. Nemkov
R. GoldsteinPublication: ASM International, 2014
Robert C. Goldstein, John K. Jackowski, Valentin S. Nemkov · IFHTSE 2014
V. Nemkov, V. Bukanin, A. Zenkov, A. Ivanov · MEP 14 Hannover, Germany
Zhichao (Charlie) Li and B. Lynn Ferguson, Valentin Nemkov, Robert Goldstein and John Jackowski, Greg Fett · ASM HTS 13 Indianapolis, IN
Kreter, Goldstein, Yakey, Nemkov · ASM HTS 13 Indianapolis, IN
V. Nemkov · HES 13 Padua, Italy
Dr. Lynn Ferguson, Dr. Zhichao Li, Dr. Valentin Nemkov, Robert Goldstein, John Jackowski, Greg Fett · HES 13 Padua, Italy
V. Nemkov, R. Goldstein, K. Kreter, and J. Jackowski · HES 13 Padua, Italy
R. Haun, M. Charles, R. Lampson, P. Meese, V. S. Nemkov, R. Goldstein, K. Kreter · HES 13 Padua, Italy
V. Vologdin, Vl. Vologdin, Jr., V. Nemkov, and K. Kreter · HES 13 Padua, Italy
Induction heating is the most progressive method for brazing of squirrel cage (SC) type rotors of electric motors. Frequencies from 3 to 10 kHz are typically being used for brazing of relatively large rotors (diameter more than 200 mm). If the ring thickness exceeds its height, flat single or two-turn inductors with concentrator are located under the ring instead of the round coil surrounding the ring. The rotor is standing on the top of the coil providing high pressure onto the joint components; a gap between the coil and ring is minimal and constant during the heating process.
This study describes a modified system with concentrator made of magnetic composite Fluxtrol 100. Frequency was much higher (around 50 kHz) than traditionally used (3-10 kHz). Electromagnetic and thermal coupled simulation with Flux 2D used to compare the process parameters and temperature distribution dynamics at 3 and 50 kHz. It was found that at higher frequency the brazing quality and time are approximately the same as at lower frequency. Electrical efficiency is slightly higher at 50 kHz while the coil current is significantly lower. Computer simulation at different powers showed that for a larger rotor the minimum required power is 70-75 kW. At lower power brazing time quickly increases and at 50 kW reaches 16 min instead of 5 min at 75 kW. Electrodynamic forces between the coil and rotor at 75 kW equal to 250 N at 50 kHz and almost 950 N at 3 kHz.
Thermal simulation of the coil proved that the maximum temperature of Fluxtrol 100 concentrator is below 200 C, which is acceptable for this material. Experimental and then industrial tests confirmed the results of simulation.
V. Nemkov, R. Ruffini, R. Goldstein, J. Jackowski, T. L. DeWeese, R. IvkovPublication: IEEE TRANSACTIONS ON MAGNETICS, VOL. 48, NO. 1
Dr. Valentin Nemkov, Mr. Robert Goldstein, Mr. John Jackowski · 26th ASM HTS Cincinnati, OH
V. Nemkov, R. Ruffini, R. Goldstein, J. Jackowski, T.L. DeWeese and R. Ivkov · HES 10/COMPEL Padua, Italy
V. Nemkov, R. Goldstein, J. Jackowski, N. Vyshinskaya, C. Yakey · HES 10 Padua, Italy
V. Nemkov, R. Ruffini, A. Kolesnichenko · EPM Dresden, Germany
Robert C. Goldstein, Valentin Nemkov and John Jackowski · 25th ASM HTS Indianapolis, IN
Valentin Nemkov, Robert Goldstein · UIE Katowice, Poland
This presentation is a continuation of the optimal design analysis of scanning process and inductors for scan hardening of axles that had been reported in 2007 in two publications [1,2] and in presentation at a conference HES-07 in Padua, Italy [3]. Improvements based on coil optimization at two frequencies (1 and 3 kHz) have been reported in these presentations. Current article describes what additional improvements may be achieved when two frequnces are used during the process of heat treating.
Vehicle axles are parts that have been induction heat treated for many years. Demands for increased vehicle reliability, fuel economy and performance have led to more challenging heat treatment specifications for axles. While being asked to produce better product, the automotive parts suppliers face an increased competition and relentless demands to lower costs.
R. Goldstein, V. Nemkov and R. MadeiraMagazine: Industrial Heating, December 2006
C. Myers, J. Osborn, C. Tiell, R. Goldstein and R. RuffiniMagazine: Industrial Heating, December 2006
Robert Ivkov, Sally J. DeNardo, Wolfgang Daum, Allan R. Foreman, Robert C. Goldstein, Valentin S. Nemkov, and Gerald L. DeNardoConference/Publication: Journal of Clinical Cancer Research 11 (19 suppl)
Methods – Thirty-seven female BALB/c athymic nude mice (5-8 weeks) were exposed to an AMF with frequency of 153 kHz, and amplitude (400-1,300 Oe), duration (1-20 minutes ), duty (15-100%), and pulse ON time (2-1,200 seconds). Mice were placed in a water-cooled four-turn helical induction coil. Two additional mice, used as controls, were placed in the coil but received no AMF exposure. Tissue and core temperatures as the response were measured in situ and recorded at 1-second intervals.
Results – No adverse effects were observed for AMF amplitudes of V700 Oe, even at continuous power application (100% duty) for up to 20 minutes. Mice exposed to AMF amplitudes in excess of 950 Oe experienced morbidity and injury when the duty exceeded 50%.
Conclusion –High-amplitude AMF (up to 1,300 Oe) was well tolerated provided the duty was adjusted to dissipate heat. Results presented suggest that further tissue temperature regulation can be achieved with suitable variations of pulse width for a given amplitude and duty combination. These results suggest that it is possible to apply high-amplitude AMF (>500Oe) with pulsing for a time sufficient to treat cancer tissue in which magnetic nanoparticles have been embedded.
R.C. Goldstein, V.S. Nemkov and R.T. RuffiniMagazine: Industrial Heating, November 2003
No matches. Try fewer filters.

Nov. 11, 2015
Energoizdat, Leningrad, 1981, 328 p., in Russian
by A.E. Slukhotsky, V.S. Nemkov, N.A. Pavlov and A.V. Bamuner
ASM International, 2014
by R. Goldstein, W. Stuehr and M. Black
by R. Goldstein
CRC Press, 2009, 740 p., edited by Cemil Gur, Jiansheng Pan
Chapter 10: Modeling of Induction Hardening Processes, pp. 427-499
by V. Nemkov
Vulkan-Verlag GmbH, 2008, 202 p.
by A. Muehlbauer
V. Nemkov: book editing, chapter 7: Design and Calculation Methods
CRC Press, 2004, 984 p. Edited by George E. Totten, Kiyoshi Funatani and Lin Xie
Chapter 15: Design Principles for Induction Heating and Hardening
by Dr. Valentin Nemkov and Robert Goldstein
UIE, “Induction Heating” working group, France, 1992, 144 p.
Chapter 1: Fundamentals
by Dr. Valentin Nemkov
Energoatomizdat, Leningrad, 1988, 280 p., in Russian by V.S. Nemkov and V.B. Demidovich
Polytechnica, Leningrad, 1991, 80 p., in Russian by V.S. Nemkov, B.S. Polevodov, and S.G. Gurevich
| Year | Inventor | Subject Matter | Patent No. |
| 2008 | Nemkov, Valentin; Madzharov, Nikolay | Sealing device for producing sealed packages of a pourable food product | AT389527T |
| 2007 | Nemkov, Valentin; Madzharov, Nikolay | Sealing device and method for producing packages of pourable food products | WO2007138372 |
| 2006 | Nemkov, Valentin; Goldstein, Robert et al. | Therapy via targeted delivery of nanoscale particles | WO2004071370 |
| 2000 | Ruffini, Robert S.; Nemkov, Valentin | Heat treating of metallurgic article with varying aspect ratios | US6166360 |
| 2000 | Nemkov, Valentin; Cherico, Stephen | High Frequency Induction Fusing | US6162509 |
| 1999 | Nemkov, Valentin; Cherico, Stephen | High Frequency Induction Fusing | ZA9806813 |
| 1984 | Ruffini, Robert S. | Inductor, coating and method | US4486641 |
Year | Company Involvement | Subject Matter | Patent No. |
|---|---|---|---|
2014 | Amass Energy LLC | Device and methods for processing carbon based materials | |
1994 | Armco Steel Company, L.P. | Induction heated meniscus coating vessel | |
1993 | Armco Steel Company, L.P. | Induction heated meniscus coating vessel | |
1996 | Avco Corporation | Method for densifying and refurbishing brakes | |
1995 | Avco Corporation | Apparatus for densification of porous billets | |
2007 | Baker Hughes Inc. | Antenna core material for use in MWD resistivity measurements and NMR measurements | |
2006 | Baker Hughes Inc. | Method and apparatus of reducing ringing in a nuclear magnetic resonance probe | |
2005 | Baker Hughes Inc. | Method and apparatus of reducing ringing in a nuclear magnetic resonance probe | |
1999 | Borg-Warner Automotive, Inc. | Clutch assembly having reaction force circuit | |
2001 | BorgWarner Inc. | Dual clutch rear axle and method of operation | |
2006 | Comaintel, Inc. | Induction heating work coil | |
2009 | Contour Hardening, Inc. | Induction driven ignition system | |
2013 | Enteroptyx | Induction heater system for shape memory medical implants and method of activating shape memory medical implants within the mammalian body | |
1995 | Essex Specialty Products, Inc. | Apparatus for heating substrate having electrically-conductive and non-electrically-conductive portions | |
2004 | European Community (EC) | Uniform gas distribution in large area plasma source | |
2001 | European Community (EC) | Method and apparatus to produce large inductive plasma for plasma processing | |
2002 | Hazelett Strip-Casting Corporation | Method, system and apparatus for continually synchronizing travelling movement of two revolving edge dams in a continuous casting machine | |
2000 | Illinois Tool Works Inc. | Multiple head inductive heating system | |
1994 | Inland Steel Company | Apparatus and method for magnetically confining molten metal using concentrating fins | |
1993 | Inland Steel Company | Apparatus and method for sidewall containment of molten metal with horizontal alternating magnetic fields | |
1993 | Inland Steel Company | Apparatus and method for magnetically confining molten metal | |
2013 | Mattson Technology, Inc. | Inductive plasma source with high coupling efficiency | |
2005 | Nexicor LLC | Method of adhesive bonding by induction heating | |
2004 | Nexicor LLC | Integral hand-held induction heating tool | |
2003 | Nexicor LLC | Hand held induction tool with energy delivery scheme | |
2003 | Nexicor LLC | Method of adhesive bonding by induction heating | |
2003 | Nexicor LLC | Hand held induction tool | |
2000 | Paragon Medical Limited | Targeted hysteresis hyperthermia as a method for treating tissue | |
2000 | Sandvik AB | Diamond coated cutting tool insert | |
1998 | Sandvik AB Megadiamond | Diamond coated cutting tool insert and method of making same | |
1998 | Textron Systems Corporation | Method for densification of porous billets | |
2007 | Veeco Instruments, Inc. | Charged particle source and operation thereof | |
2011 | Devices for targeted delivery of thermotherapy, and methods related thereto | ||
2010 | Aduro Biotech | Magnetic nanoscale particle compositions, and therapeutic methods related thereto |
Talk with a Fluxtrol engineer about your coil, material or heat pattern challenge.